During the process of carrying out Internal Quality Control the clinical laboratory professional faces several challenges in the critical analysis process, mainly related to system alerts that indicate a situation of non-compliance.
Knowing how to deal with loss of control and what actions should be taken is essential to guarantee test results.
Critical analysis represents the sixth step of the "Internal Quality Control (IQC) Journey", a system consisting of nine steps to ensure that analytical processes function correctly and that results are delivered safely.
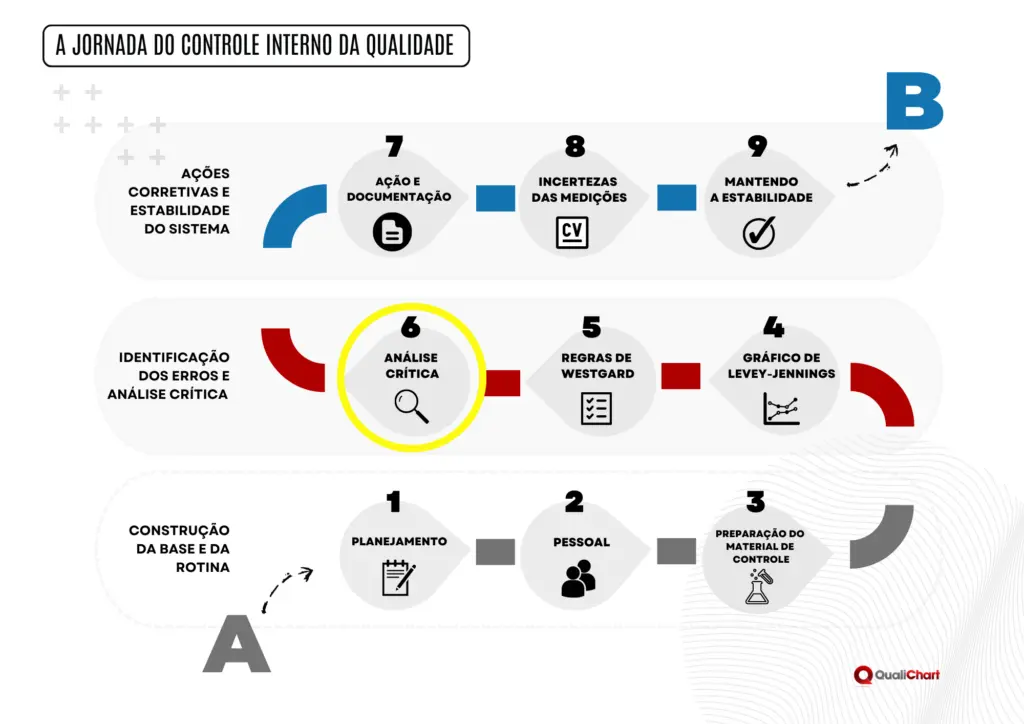
The IQC journey is an online guide that clearly and simply shows the steps necessary to face the challenges of internal quality control, such as validating control daily, performing critical analyzes correctly, applying multiple rules and managing the team and staff turnover.
If you don't already know the steps, you can access our guide by clicking hereand have access to all the information necessary to successfully follow the IQC journey.
In this content we will see how to develop a strategy to deal with the loss of control and what are the seven actions to be taken.
7 fundamental attitudes:
- Inspect control chart in detail
- Analyze possible causes of errors
- Perform interventions in the system, aiming to correct the problem
- Note the measures taken to correct the problem
- Perform new analytical run, for control and patient samples
- Test the new data
- Interpret the result of the last assessment and decide on referral
In a control noncompliance situation, the laboratory must determine a root cause for the OUTLIER data and how to adapt a possible correction.
OUTIER is an atypical addition that presents great value or other series information (which is big news or which is inconsistent.)
The quality control method adopted must be able to find problems with a minimum of false rejections, being able to alert when there are problems and not disturb if the system is stable.
During a loss situation, many professionals carry out all sorts of controls, be it control, new rate of material, in short, an action that appears objective and is immediately within reach. Caution must be exercised at this time, as taking these actions can be considered a random attitude, devoid of foundation and rational basis, and therefore less decisive.
Having a strategy constitutes a very important focus on the root cause, and thus, more chances of adopting an effective corrective measure.
Attitudes such as repeating the control run, without analyzing the situation, are not a good practice for a laboratory that plans and takes care of quality strategies. Although it occurs in the same way, the result cannot be caused by degradation of the vial of control material itself, that is, it cannot be used from that moment on in the vial. Taking care of the material bottle and its proper conservation are essential. In this case, opening a new bottle may be an effective measure and should be documented in run comments. It is worth highlighting that this attitude is a rational attitude and is part of the actions to be implemented as part of a rational coping strategy for the OUTLIER situation.
If quality control is well planned, and the Quality Manager expands his knowledge test by test, his vision of analytical systems will be so consistent that it will enable clarity and greater accuracy in the search for solutions.
Solving control problems requires knowledge and attitudes. It is up to the laboratory quality manager, a higher-level professional, to discover the causes and solve the problems.
1. Inspect the control chart in detail
The visual interpretation of the control chart can be very enlightening. We can infer whether there is a trend, which indicates the type of systematic error or whether the distribution of points suggests a random nature. Violated rules also provide important indicators of the type of error.
Rules that evaluate consecutive control observations, such as 2:2s, 4:1s, 7x, 10x and 7T usually indicate systematic error. Rules that test for broadening of the Gaussian distribution of control measurements, such as 1:3s, R:4s generally indicate random error.
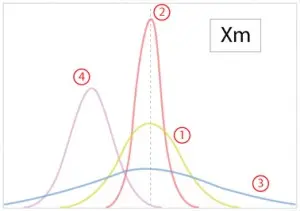
The control chart is a visual representation of the variability of results obtained from material analyses. Figure 1 shows the combination of images of the Gauss curve (positioned in counterclockwise rotation) with the control chart. Based on this principle, we can interpret the graph alongside.
Curve 1 – green – shows a Gaussian distribution of results, with an acceptable shape and an adequate average. The coefficient of variation would be at values less than the maximum imprecision allowed for the test.
Curve 2 – red – very good variability (small), showing distribution of values closest to the average. The CV should be comfortably below the maximum allowable imprecision.
Curve 3 – blue – the Gaussian distribution appears wide, indicating very dispersed results, even though they remain equidistant from the average value. Indicates random errors.
O control chart is an essential tool in quantitative internal control and the professional must become familiar with it. It provides a lot of information and has a great pedagogical effect, allowing information about control events to be shared with all employees. It is good control practice to always inspect the Levey-Jennings chart. The practice of simply comparing the result of the run with a range recommended by the manufacturer of the control material is a fragile criterion with a low rate of problem detection. For example, a deviation from the mean caused by loss of calibration (curve 4, above) may not be detected for many days, simply by comparing the result with a range. Analyzing the control chart, or testing the rules (e.g., 4:1s rule) reveals the problem you can solve. This is what is expected from a control system.
2. Analyze possible causes of errors
Once the type of error has been identified, whether random or systematic, go in search of the root cause. Systematic errors are more frequent, caused by persistent problems and are easier to resolve. Random errors do not have a defined meaning or direction, and are therefore more difficult to find the root cause.
Remember to check the last movement in relation to the device (recent maintenance), reagent (new reagent, new batch), calibration, etc. Use information about types of errors, in a list, to remind you of the possibilities. Carry out an accurate review of the causes of error. Spend a little time on the analysis, to save on time and materials, avoiding fruitless repetitions that increase your costs. Mainly evaluate two aspects:
- If the problem affects other tests that are performed on the same device. This is what we can call a “common denominator” for the different analytical systems.
- If there has been recent intervention on the equipment, from preventative maintenance, any damage, to changing reagents.
3. Perform interventions on the system to correct the problem
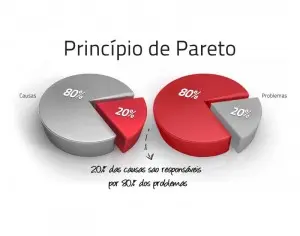
Evaluate and learn about your analytical system and its performance. Use records of nonconformities for the analyte as a way to recall other violations – even old ones – to detect possible recurrences of the same problem. Consider the option of analyzing the nonconformities, root causes and corrective measures previously adopted. Remember the Pareto Principle, which establishes that 80% of problems have less than 20% of causes. It is a valid axiom for the IQC in clinical laboratory.
Avoid simply replacing the vial of control material, or using new reagent, which may supposedly give faster results. In fact, it may be that we are just postponing effective measures. However, it is always possible that an analyte has deteriorated in a material during use and by analyzing another vial it will be possible to find the solution to the problem, which in this case would be in the material that has the function of controlling the stability of the system, but which itself would have lost stability. This deterioration may be caused by poor conservation of the material.
4. Note the measures taken to correct the problem
Having the habit of always recording is of great importance. Only then will you be able to better solve future problems with the same analytical system, as advocated in the previous item. In automated computer control systems, look for the form of recording in 'Comments', or 'Observations' in the analytical run, to note the interventions, or also write down some other type of information regarding the analytical system.
Recording each corrective action will provide you with a source for queries about errors and corrections in that analytical system. You may find it appropriate to repeat a previously adopted corrective measure that was successful. For the analytical run, make it a habit to also note down observations on interventions in the system, of other types, such as preventive maintenance, batch changes of reagents, calibrations, needle changes, etc. Often a simple and apparently innocent intervention can be associated with the cause of the problem found. Anyone who carries out quality control only with the equipment's own module has to make these notes in separate records, which is always more laborious.
5. Perform new analytical run, for control and patient samples
If the criterion was rejection of the analytical run, a new run must be carried out for the control levels of the analyte(s), after having taken rationally defined steps to review the analytical system and correct any problems found. This repetition is not meaningless, because it aims to verify whether the measure adopted was in fact sanitary and resolving. If the problem factor remains, it will continue to negatively influence the results of controls and would also influence those of patients. Without a careful assessment of the root cause and appropriate corrective measures, repetition will only delay the identification of problems and the effective application of corrective measures.
Be careful with the behavior of just repeating control analysis. With simple and automatic repetition, without a rational basis for evaluating the cause, you are saying that you do not trust that the control system fulfills its role of being able to detect problems. Especially in the case ofrandom errors, repeating the analysis of controls can, due to the analytical variation inherent to the method, produce results ‘in control’ without there having been an effective correction of any problem. If the treatment criterion for the nonconformity was rejection, you must perform a new run for all implemented levels, even if the rejection was motivated by just one of them. The interpretation is that the analytical run was rejected and consequently all control levels analyzed in that run must be rejected. Performing a new run is very important and necessary to do, ALWAYS after analyzing the possible causes.
6. Test the new data
The control method you use (computer program) must allow you to enter a new analytical run value, replacing the previous ones, if there is rejection. After entering the new values, all enabled rules must be tested and the graph plotted. The original value that caused a rule violation must be preserved in the record and made available for history and review for each analyte.
The value that caused the violation remains archived, but is not used for calculations of current values, for interpretation of the Coefficient of Variation. This is because you adopted the rejection criteria for the run, and you must include new data that is accepted. Archiving the data that generated the non-conformities serves to document the IQC performance and in subsequent reviews, to guide reasoning about recurrences of the same problem. If a problem is recurring, you must take care to establish further analysis to adopt preventive measures. Consider holding a discussion with the equipment's technical consultant, or with the reagent manufacturer's SAC.
7. Interpret the result of the last assessment and decide on referral
It is very important that the solution to the problem did not occur by chance, but rather as a result of your intervention in the system. If the last result is in control, you have the support to consider that patient samples will have results with analytical quality if they are treated in a similar way to the control material. If there is persistence of OUTLIER with a second result you must be even more careful and review the entire system. You should check the CHECK LIST of causes of errors and try to open your thinking to look for other possible causes that have not yet been identified. If you use a computer program for IQC, you must activate the program'sError Assistantto receive assistance in finding the causes.
Whenever triggered by its employees in a situation of persistent nonconformity, the Quality Manager must analyze the problem, adopting a systemic view of the analytical process, with criteria.
- Must inspect the control chart, the rules violated and the type of error, whether random or systematic. Through this analysis it is possible to classify the type of error, or with the help of the program. Systematic errors show trend. These are changes that occur gradually over time. Random errors point to greater variability in the system, and mean a broadening of the distribution curve of control results, or the Gauss Curve;
- Relate the type of error with the potential causes. Systematic errors and random errors have different causes. Problems that cause systematic errors are more common than those that cause random errors;
- Must consider other analytes in multiple test system. If there are also problems with these others, the analysis must continue in relation to the characteristics of the tests, the equipment, the filters, lamp, that is, what could be in common;
- Relate the problem to recent interventions. Systematic errors are often related to reagent and calibration problems. One marked deviation from the mean may be due to reagent change, change Lot , recent calibration, calibrator lot change. These are interventions that, when carried out, must be noted in the internal control method (computer program), to guide root cause analyzes of nonconformity;
- Record measures taken. Always register, so you can consult later. Note the corrective measure in an appropriate place, if it was indeed a factor in the solution.
Develop good habits and share them with your team. Good attitudes are incorporated into people's daily lives and translate into appropriate referrals naturally. This increases the effectiveness of your internal control and confidence in your systems and their results.